
- Catalogs
- Monmouth Scientific
- Circulaire® Access Recirculating Fume Cupboard


Circulaire® Access Recirculating Fume Cupboard
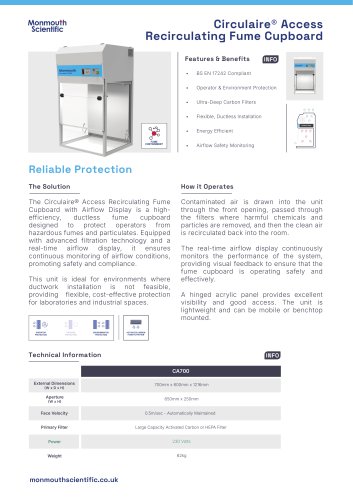
Circulaire® Access Recirculating Fume Cupboard
The Circulaire® Access Recirculating Fume Cupboard is a high-efficiency, ductless unit designed to protect operators from hazardous fumes and particulates. It features advanced filtration technology and a real-time airflow display for continuous monitoring, ensuring safety and compliance. This unit is ideal for environments where ductwork installation is not feasible, offering flexible and cost-effective protection for laboratories and industrial spaces.
Contaminated air is drawn into the unit through the front opening, filtered to remove harmful chemicals and particles, and then recirculated back into the room. The real-time airflow display provides visual feedback to ensure safe and effective operation. The unit is lightweight and can be either mobile or benchtop mounted.
- BS EN 17242 Compliant
- Operator & Environment Protection
- Ultra-Deep Carbon Filters
- Flexible, Ductless Installation
- Energy Efficient
- Airflow Safety Monitoring
- External Dimensions: 700mm x 600mm x 1216mm
- Aperture: 650mm x 250mm
- Face Velocity: 0.5m/sec - Automatically Maintained
- Power: 230 Volts
- Weight: 62kg
- Primary Filter: Large Capacity Activated Carbon or HEPA Filter
The unit features a compact construction ideal for spaces without exhaust systems, making installation easier and more versatile. It is fully compliant with BS EN 17242 and COSHH regulations, featuring integral lighting, low airflow alarm, hinged acrylic front panel, cable ports, and top & rear baffles.
- Static Base Stand with Adjustable Feet
- Mobile Base Stand with Lockable Castors
- Filter Condition Alarm
- Gas & Water Services
The system uses Activated Carbon and/or HEPA Filters to provide complete protection against hazardous substances. The digital airflow monitor with an animated colour LCD enhances user safety and reduces downtime.
Catalog excerpts
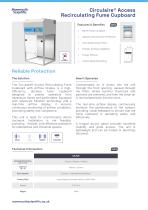
Circulaire® Access Recirculating Fume Cupboard Features & Benefits ■ Operator & Environment Protection ■ Ultra-Deep Carbon Filters ■ Flexible, Ductless Installation ■ Airflow Safety Monitoring Reliable Protection The Solution The Circulaire® Access Recirculating Fume Cupboard with Airflow Display is a high-efficiency, ductless fume cupboard designed to protect operators from hazardous fumes and particulates. Equipped with advanced filtration technology and a real-time airflow display, it ensures continuous monitoring of airflow conditions, promoting safety and compliance. This unit is ideal for environments where ductwork installation is not feasible, providing flexible, cost-effective protection for laboratories and industrial spaces. Co ntaminated air is drawn into the unit t hrough the front opening, passed through the filters where harmful chemicals and particles are removed, and then the clean air is recirculated back into the room. The real-time airflow display continuously monitors the performance of the system, providing visual feedback to ensure that the fume cupboard is operating safely and effectively. A hinged acrylic panel provides excellent visibility and good access. The unit is lightweight and can be mobile or benchtop mounted. Technical Information
Open the catalog to page 1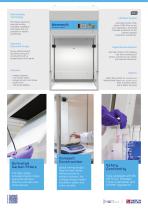
Eliminates expensive external ducting, simplifies installation, and makes the unit portable for flexible positioning. Monmouth Circulaire® Access Filtration System Activated Carbon Filter and/or HEPA Filter to suit your application, providing complete protection for the operator against hazardous substances. Improved Structural Design Epoxy painted steel & aluminium extrusion construction with a hinged acrylic front panel. Features - Integral Lighting - Hinged Acrylic Front Panel - Cable Ports Digital Airflow Monitor Animated Colour LCD displays real-time monitoring of airflow, enhancing user...
Open the catalog to page 2All Monmouth Scientific catalogs and technical brochures
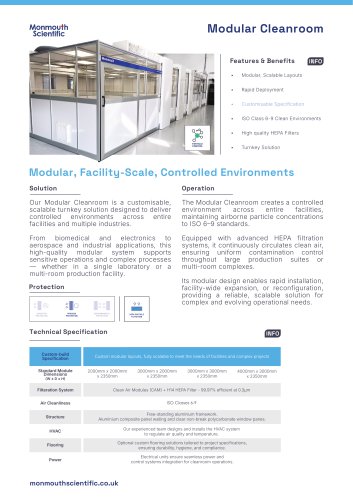 Modular Cleanroom
2 Pages
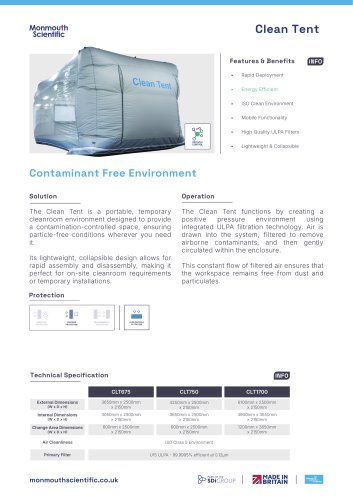 Clean Tent
1 Page
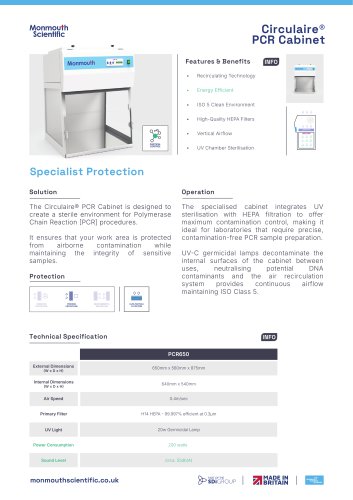 Circulaire® PCR Cabinet
1 Page
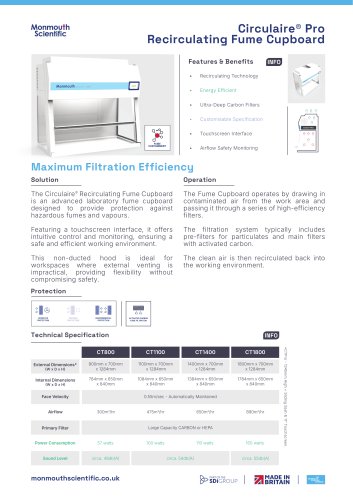
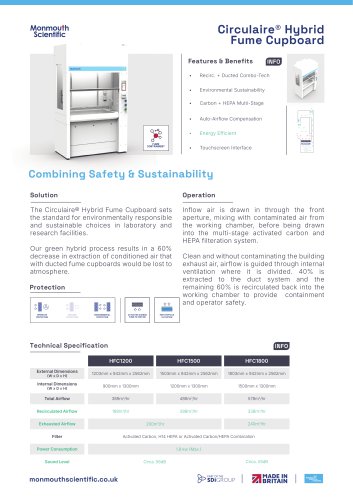
- 2 doors wardrobe
- 1-door wardrobe
- Laboratory hood
- Laboratory cabinet
- White cabinet
- Laboratory workstation
- Biosafety cabinet
- Laboratory biosafety cabinet
- Benchtop fume hood
- Chemical fume hood
- Class II biosafety cabinet
- Laboratory material cabinet
- Laboratory bench
- Floor-standing fume hood
- Microbiological safety cabinet with HEPA filter
- Cabin
- Stainless steel fume hood
- Ventilated cabinet
- Benchtop laboratory workstation
- HEPA hood